Industry Knowledge & Insights

Frain Machinery Blog

Latest Articles, Buying Guides, and Rental Strategies for Packaging & Processing

0%

Choosing Pharmaceutical Capping Machinery is not merely a question of speed. It is a decision about closure integrity, repeatability, and the realities of a production floor. Grand View Research’s Pharmaceutical Packaging Market Size, Share & Trends Analysis Report estimated the global market at USD 133.4 billion in 2023. That broader market figure does not predict demand for any single capper, but it signals the scale of packaging operations manufacturers must support. A forecast is not a machine specification.

The right choice depends on the container, closure, and line conditions. A bottle may need a screw cap, child-resistant closure, or tamper-evident seal. Each changes the handling and torque requirements. FDA 21 CFR 211.130 requires packaging operations to use controls that prevent mix-ups and ensure correct labeling. In practice, buyers should also assess changeover time, cap feeding, torque control, cleaning access, and integration with upstream filling and downstream inspection. Small details matter. A cap that looks secure may still be inconsistently applied.

W. Edwards Deming, a quality-management expert, is commonly associated with the principle, “Quality is everyone’s responsibility.” It applies here: operators, maintenance teams, and quality staff all influence closure performance. Ask suppliers for test data using your actual bottles and caps, not only catalog specifications. A line-speed claim alone can mislead. This guide examines the practical criteria for choosing Pharmaceutical Capping Machinery, while recognizing that no checklist replaces a properly designed production trial.
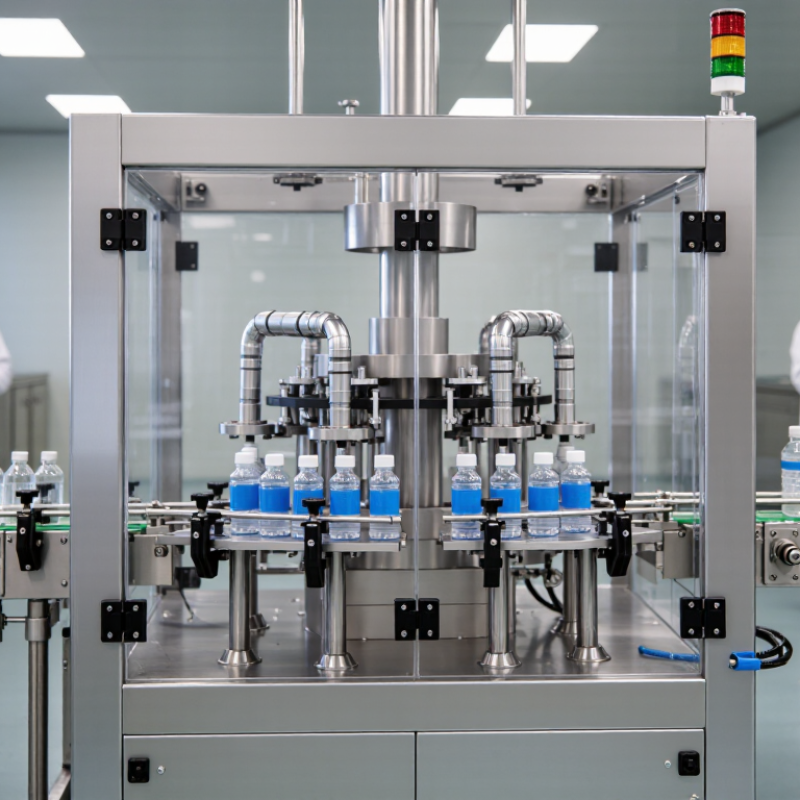
How to Choose Pharmaceutical Capping Machinery

Define Product and Closure Requirements Under 21 CFR Part 211

Choosing a pharmaceutical capper starts with the product and closure, not the machine’s advertised speed. Record bottle material, neck finish, cap type, liner, and the validated application-torque range.

Grand View Research’s 2023 Pharmaceutical Packaging Market report valued the global market at USD 124.9 billion in 2022 and forecast 9.6% annual growth through 2030. That market estimate is context, not a specification; your own container-closure system must drive equipment selection.

Fit matters.

Under 21 CFR 211.130, packaging and labeling operations must prevent mix-ups, while 211.122 and 211.125 require controls for labeling materials and their issuance. Choose machinery that supports documented setup, controlled changeovers, and clear batch records. Check whether operators can verify cap presence, closure height, and torque without stopping the line unnecessarily.

Not just speed.

FDA’s 21 CFR 211.100 also requires written production procedures and documented deviations. A torque target can look tidy on paper, yet cap behavior may shift with bottle finish, liner compression, or line speed. Test representative containers at operating conditions, retain the results, and define acceptable limits before routine production.

One detail is easy to miss: the best setting may not be the easiest one to reproduce across shifts.

Match Capping Technology to Closure Type and Required Bottles per Minute

How to Choose Pharmaceutical Capping Machinery

Match Capping Technology to Closure Type and Required Bottles per Minute

Start with the closure, not the machine catalogue. Threaded plastic caps often suit spindle or chuck cappers, while snap-on closures need controlled vertical pressure. Aluminum roll-on closures require forming heads that shape the skirt around the bottle finish. These methods are not interchangeable. A cap that looks secure may still leak if its liner, thread, or application force is mismatched.

Then calculate the real production rate. A line targeting 120 bottles per minute needs more than a capping head rated for 120. Allow for cap feeding, brief stops, bottle spacing, and downstream equipment. Check performance using the actual bottle and closure. Small changes in bottle height or cap friction can affect torque and reject rates. Watch the line during a sustained run, not just a short demonstration. That matters.

Ask how operators will adjust torque, change closure sizes, and clear jams. Review cap orientation and feeding, too; poorly presented caps can limit output even when the capping station is fast. Record applied torque and inspect samples for cross-threading, loose caps, and damaged finishes. A tidy specification sheet can still mislead. Production conditions are less tidy. Choose equipment that meets the needed rate with stable closure quality, and leave room for sensible changeovers.

How to Choose Pharmaceutical Capping Machinery

Match capping technology to closure type and required bottles per minute.

Bars show indicative throughput ranges, not guaranteed machine ratings. Screw and press-on caps commonly use rotary or inline cappers; ROPP caps require roll-on heads, while vial crimp seals require crimping equipment. Confirm the required rate against the container, closure, feeding system, and line configuration.

Set Torque and Seal-Test Limits from Product-Specific Validation Data

How to Choose Pharmaceutical Capping Machinery

Set Torque and Seal-Test Limits from Product-Specific Validation Data

Choose capping machinery that can repeatedly meet limits established for your product. Use validation data from the actual container, closure, liner, and filling conditions. Record the acceptable application and removal torque ranges, not just one target value. Too little torque may allow leakage; too much can damage threads or make opening difficult. Small differences matter. Confirm settings across normal line speeds and planned operating shifts.

Set seal-test limits using a method suited to the package and product. Define acceptance criteria before qualification runs, then test samples from startup, steady production, and changeovers. Track torque and seal results together. A passing torque reading alone does not prove a reliable seal. If results drift, check cap alignment, chuck wear, container variation, and environmental conditions before changing settings. Validation can expose awkward trade-offs; document them rather than forcing a neat but unsupported limit.

Tips: Keep calibrated torque tools and seal-test equipment available. Retain raw results, including failures. Review limits after meaningful changes to components or process settings, and revalidate when needed.

Assess GMP Compliance Against ISO 15378:2017 and 21 CFR Parts 210–211

ISO 15378:2017 applies to primary packaging materials for medicinal products and incorporates GMP principles. 21 CFR Parts 210–211 set U.S. drug manufacturing requirements. Capping machinery does not make a facility compliant by itself. Its design, operation, records, and maintenance must fit the site’s quality system.

Ask how the machine supports documented controls. Can operators set and verify cap torque within approved limits? Are torque readings, alarms, rejects, and adjustments recorded and reviewable? Check calibration records, cleaning instructions, change control, and component traceability. Look for clear procedures for line clearance and handling rejected caps. Ask for qualification evidence, including installation and operational testing, and confirm that performance testing reflects your actual closures and containers. Small details matter.

A machine may apply consistent torque yet fail to detect a damaged liner. That assumption deserves scrutiny. Review how deviations are investigated and whether electronic records have suitable access controls and audit trails. Requirements depend on intended use and facility procedures, so involve quality and engineering staff before purchase. A tidy demonstration is not enough. Request evidence from sustained runs, not only a short sample. Recheck the fit when containers, closures, or settings change.

How to Choose Pharmaceutical Capping Machinery - Assess GMP Compliance Against ISO 15378:2017 and 21 CFR Parts 210–211

Assessment Dimension What to Evaluate Relevant Standard or Regulation Objective Evidence to Request or Review
Equipment design and suitability Confirm the capper is appropriately designed, sized, and located for its intended operation; product-contact and container-contact parts should be suitable for the process and accessible for cleaning and maintenance. 21 CFR 211.63; ISO 15378:2017 provides a quality-management and GMP framework for primary packaging material manufacturers. Equipment specifications, layout drawings, material specifications, intended-use assessment, and documented design or installation review.
Cleaning and maintenance Check that written procedures define cleaning, inspection, and maintenance, including responsibilities, frequency, and records. Assess whether change parts and contact surfaces can be cleaned effectively. 21 CFR 211.67; ISO 15378:2017 operational controls and documented-information framework. Approved cleaning and maintenance procedures, completed logbooks, preventive-maintenance records, and cleaning verification or validation records where required by the process.
Controls for automated equipment For automated or electronic controls, assess whether operating limits, access, checks, and records are appropriate to the system and its use. Evaluate backup arrangements for relevant data. 21 CFR 211.68. Electronic-record requirements may also involve 21 CFR Part 11 when applicable. Functional specifications, user-access controls, alarm and event records, backup and recovery procedures, and documented testing of computerized functions.
Cap application and process control Determine whether critical settings—such as torque, speed, and reject limits—are defined and controlled for the container-closure system. Confirm that the process consistently meets approved specifications. 21 CFR 211.100 and 211.110; 21 CFR 211.165 applies to testing and release of finished drug products. Approved operating ranges, process qualification or validation records as appropriate, in-process check records, deviation investigations, and acceptance criteria for closure performance.
Container-closure component controls Verify that caps and other packaging components are handled, identified, examined, and controlled under written procedures. Confirm that the capper is compatible with the specified component and container formats. 21 CFR 211.122; ISO 15378:2017 is specifically relevant to quality systems for primary packaging materials. Component specifications, receipt and status records, line-clearance records, format-change instructions, and documented compatibility or setup checks.
Packaging-line operation Assess procedures for line setup, clearance, operation, and prevention of mix-ups. Check that packaging operations and their controls are documented. 21 CFR 211.130; related written procedures under 21 CFR 211.100. Packaging batch records, line-clearance checklists, equipment setup records, reconciliation records where applicable, and records of rejected or diverted units.
Personnel qualification and training Confirm that personnel who operate, clean, maintain, or troubleshoot the capper have relevant training and understand applicable procedures. 21 CFR 211.25; ISO 15378:2017 addresses competence and training within its management-system framework. Role-based training records, qualification records where used, and documented training on current operating and cleaning procedures.
Quality-system oversight and change control Evaluate how equipment changes, software updates, repairs, deviations, and recurring problems are assessed and approved before return to routine use. 21 CFR 211.100 and 211.192; ISO 15378:2017 includes quality-management-system controls for operation, evaluation, and improvement. Change-control records, deviation and investigation reports, corrective-action records, approval documentation, and post-change testing or requalification records as appropriate.

Scope note: ISO 15378:2017 specifies quality-management-system requirements for organizations manufacturing primary packaging materials for medicinal products; it is not, by itself, a certification standard for capping machinery. Use it as a relevant supplier or process-system benchmark where applicable, and assess the equipment against the applicable GMP requirements and the intended manufacturing process.

Compare FAT/SAT Results for Throughput, Reject Rate, and Changeover Time

When choosing pharmaceutical capping machinery, compare FAT and SAT using the same container, closure, speed setting, and measurement window. Record good units per minute, rejects per thousand, and minutes required for a format change. Count start-up losses and adjustments, not only the stable production run. Small details matter.

The OEE Industry Standard benchmark commonly describes 60% as typical manufacturing performance and 85% as world-class. Treat these figures as broad context, not a pharmaceutical acceptance limit. A capper’s throughput should be judged against its agreed operating conditions. Separate mechanical stops from upstream supply interruptions, and classify rejects by cause, such as loose caps, damaged closures, or misaligned application. FDA’s Process Validation guidance (2011) emphasizes documented evidence across equipment qualification and ongoing process monitoring. A test record should therefore preserve settings, sample sizes, timestamps, and operator interventions.

At SAT, repeat the FAT protocol on the installed line, with actual feeding and downstream handling. Compare changeover time from the last acceptable unit of one format to the first acceptable unit of the next. That definition prevents optimistic stopwatch results. A short test can flatter performance. It may miss jams that appear only after prolonged running, or small losses during cap replenishment. Keep the raw counts. Review outliers before deciding whether a gap reflects the machine, the line, or the test itself.

FAQS

What information should guide pharmaceutical capper selection?

Start with the bottle material, neck finish, cap type, liner, and validated application-torque range. Fit matters.

Why isn’t advertised speed enough to choose a machine?

Speed alone does not show closure quality or repeatability. Test representative bottles at operating conditions and record the results.

What production controls should the machine support?

It should support documented setups, controlled changeovers, batch records, and checks for cap presence, closure height, and torque.

Does capping equipment alone ensure GMP compliance?

No. Its design, operation, records, and maintenance must fit the facility’s quality system. A tidy demonstration is not enough.

What records should buyers review before purchase?

Review calibration, cleaning, maintenance, change-control, traceability, and qualification records. Check how alarms, rejects, torque readings, and adjustments are documented.

How should FAT and SAT performance be compared?

Use the same container, closure, speed, and measurement window. Record good units per minute, rejects per thousand, and changeover minutes.

What should a realistic changeover-time measurement include?

Measure from the last acceptable unit of one format to the first acceptable unit of the next. Include adjustments and startup losses.

Why repeat testing during sustained production?

Longer runs may reveal jams or losses during cap replenishment. Short tests can flatter performance. Keep raw counts and review outliers.

Conclusion

Choosing Pharmaceutical Capping Machinery starts with clearly defining the product, bottle, and closure requirements, including the controls needed to maintain consistent packaging under 21 CFR Part 211. The selected capping technology should suit the closure type and reliably meet the required bottles-per-minute rate without compromising container integrity. Torque settings and seal-test limits should come from product-specific validation data, rather than assumptions, so acceptance criteria reflect the actual package and process.

Before purchase, assess whether the equipment supports applicable GMP expectations under ISO 15378:2017 and 21 CFR Parts 210–211. Review documented factory and site acceptance test results to confirm throughput, reject rate, and changeover time under representative operating conditions. A structured comparison of these results, along with clear validation and maintenance requirements, can help determine whether the machinery is suitable for the intended production process.
Lily

Lily

Lily is a dedicated marketing professional with a profound expertise in her field, bringing a wealth of knowledge and experience to our company's core operations. With a keen understanding of our product offerings, she excels in crafting compelling and insightful content that resonates with our......